

Hey there! As a supplier of space conveyors, I've been getting a lot of questions lately about the emergency response mechanisms of these high - tech machines. So, I thought I'd take a moment to share some insights on this crucial topic.
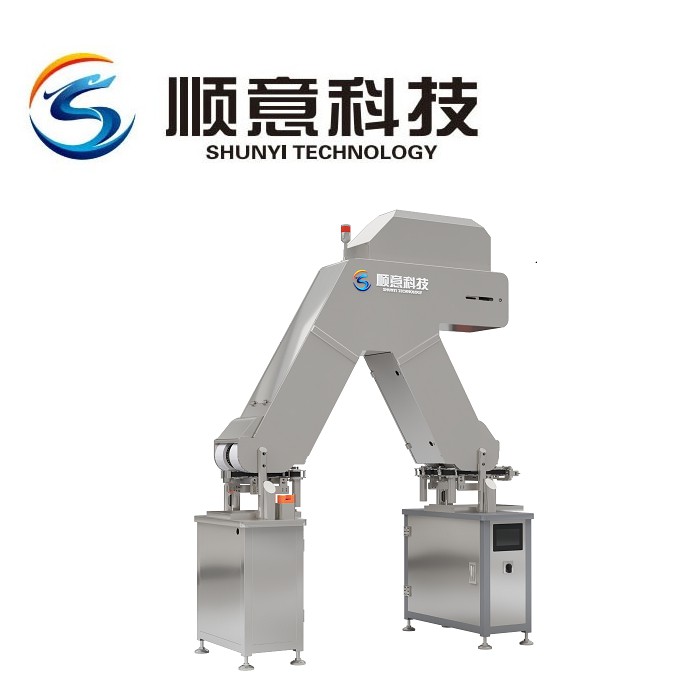
First off, let's understand what a space conveyor is. A space conveyor is a specialized system designed to move materials in unique environments, such as in pharmaceutical clean areas. We offer products like the Pharmaceutical Clean Area Elevator Conveyor and the Pharmaceutical Clean Area Space Conveyor, which are tailored to meet the strict requirements of the pharmaceutical industry.
Now, onto the emergency response mechanisms. These are put in place to ensure the safety of the conveyor system, the materials it's transporting, and the people working around it.
Sensor - Based Detection
One of the primary emergency response mechanisms is sensor - based detection. Our space conveyors are equipped with a variety of sensors that constantly monitor the system's operation. For example, there are proximity sensors that can detect if an object is too close to the conveyor belt. If a worker accidentally gets too near, the sensor will immediately send a signal to the control system.
There are also load sensors that measure the weight of the materials on the conveyor. If the load exceeds the recommended capacity, the sensor will trigger an alarm and may even stop the conveyor to prevent damage. Temperature sensors are another important component. In a pharmaceutical clean area, maintaining the right temperature is crucial. If the temperature goes out of the acceptable range, the sensor will alert the system, and appropriate actions can be taken, such as adjusting the cooling or heating systems.
Automatic Shutdown
When a serious issue is detected, an automatic shutdown mechanism kicks in. This is a fail - safe measure to prevent further damage. For instance, if there's a mechanical failure, like a broken belt or a jammed roller, the conveyor will automatically stop. This not only protects the equipment but also reduces the risk of injury to workers.
The automatic shutdown can be triggered in different ways. In addition to sensor signals, there are also emergency stop buttons located at various points along the conveyor. If a worker notices a problem, they can press the emergency stop button, and the conveyor will come to an immediate halt.
Backup Power Systems
In a space conveyor, power is essential. That's why we install backup power systems. In the event of a power outage, these backup systems can keep the conveyor running for a limited time. This is especially important in a pharmaceutical clean area, where interruptions in the material handling process can lead to product contamination or loss.
The backup power systems can be in the form of batteries or generators. Batteries are often used for short - term power supply, while generators can provide power for a longer period. They are designed to seamlessly take over when the main power source fails, ensuring that the conveyor can continue its operation until the power is restored.

Remote Monitoring and Control
We also offer remote monitoring and control capabilities for our space conveyors. Through a dedicated software system, operators can monitor the conveyor's performance from a remote location. They can check the status of sensors, view real - time data on temperature, load, and speed, and even control the conveyor's operation.
In case of an emergency, operators can quickly respond without having to be physically present at the conveyor site. They can shut down the conveyor, adjust settings, or receive alerts on their mobile devices. This feature is extremely useful, especially for large - scale pharmaceutical facilities where multiple conveyors are in operation.
Emergency Communication
Effective communication is key during an emergency. Our space conveyors are integrated with an emergency communication system. When an alarm is triggered, it not only alerts the control system but also sends notifications to relevant personnel. This can include maintenance teams, supervisors, and safety officers.
The communication can be in the form of emails, text messages, or push notifications on mobile apps. This ensures that everyone who needs to know about the emergency is informed promptly, and they can take appropriate actions.
Maintenance and Training
To ensure the proper functioning of the emergency response mechanisms, regular maintenance is essential. We provide detailed maintenance schedules and guidelines for our customers. Our technicians can also conduct on - site inspections and perform necessary repairs and replacements.
In addition, we offer training programs for the operators and maintenance staff. These programs cover the operation of the conveyor, the emergency response mechanisms, and how to handle different types of emergencies. By training the personnel, we can minimize the response time and reduce the impact of emergencies.
Customization for Different Environments
We understand that different industries and environments have different requirements. That's why our emergency response mechanisms can be customized. For example, in a pharmaceutical clean area, the requirements for cleanliness and sterility are very high. So, our conveyors are designed with features that prevent the accumulation of dust and contaminants during an emergency.
We can also customize the sensors, backup power systems, and communication channels based on the specific needs of the customer. Whether it's a small - scale laboratory or a large - scale manufacturing plant, we can tailor the emergency response mechanisms to fit the environment.
Why Choose Our Space Conveyors?
Our space conveyors are not only equipped with state - of - the - art emergency response mechanisms but also offer high - quality performance. We use the latest technology and materials to ensure the reliability and durability of our products.
The Pharmaceutical Clean Area Elevator Conveyor and the Pharmaceutical Clean Area Space Conveyor are designed to meet the strictest industry standards. They are easy to install, operate, and maintain, and they come with excellent after - sales support.
If you're in the market for a space conveyor, I highly recommend considering our products. We're committed to providing the best solutions for your material handling needs. Whether you have questions about the emergency response mechanisms or any other aspect of our conveyors, don't hesitate to reach out. We're here to help you make the right choice and ensure a smooth and safe operation of your conveyor system.
In conclusion, the emergency response mechanisms of a space conveyor are a combination of advanced technology, safety features, and effective communication. By having these mechanisms in place, we can minimize the risks associated with conveyor operation and ensure the safety of the equipment, materials, and personnel. If you're interested in learning more about our space conveyors or discussing your specific requirements, please get in touch with us. We look forward to working with you to find the perfect solution for your business.
References
- Industry standards for pharmaceutical clean area equipment
- Technical manuals for space conveyor systems