

Hey there! As a supplier of intelligent conveyors, I've seen firsthand how product jams can be a real headache in manufacturing and production lines. It can slow down operations, cause damage to products, and even lead to costly downtime. But don't worry! Our intelligent conveyors are designed to prevent these jams and keep your production running smoothly. In this blog, I'll break down how our intelligent conveyors achieve this.
1. Smart Sensors and Monitoring
One of the key features of our intelligent conveyors is the use of advanced sensors. These sensors are strategically placed along the conveyor belt to constantly monitor the flow of products. They can detect various parameters such as the speed of the products, their position, and the distance between them.
For example, infrared sensors can be used to detect the presence of products on the conveyor. If a product stops moving or gets too close to another one, the sensors will immediately pick up on this. Ultrasonic sensors can measure the distance between products, ensuring that there's always a safe gap to prevent collisions.
Once the sensors detect an issue, they send a signal to the conveyor's control system. This system can then make real - time adjustments to the conveyor's speed or direction. If there's a potential jam forming, the conveyor can slow down or even stop to give the products time to space out properly.
2. Adaptive Conveyor Speed
Our intelligent conveyors are not stuck at a fixed speed. They can adjust their speed based on the flow of products. When the production line is running smoothly and there's a steady stream of products, the conveyor can operate at a high speed to maximize efficiency.
However, if the sensors detect that products are starting to bunch up, the conveyor will automatically slow down. This gives the products more time to move along the belt without getting jammed. For instance, in a pharmaceutical production line where Empty Ampoule Convey Line is used, the conveyor can adapt its speed according to the filling and packaging process. If the filling machine is running a bit slow, the conveyor will slow down to match the pace, preventing ampoules from piling up.
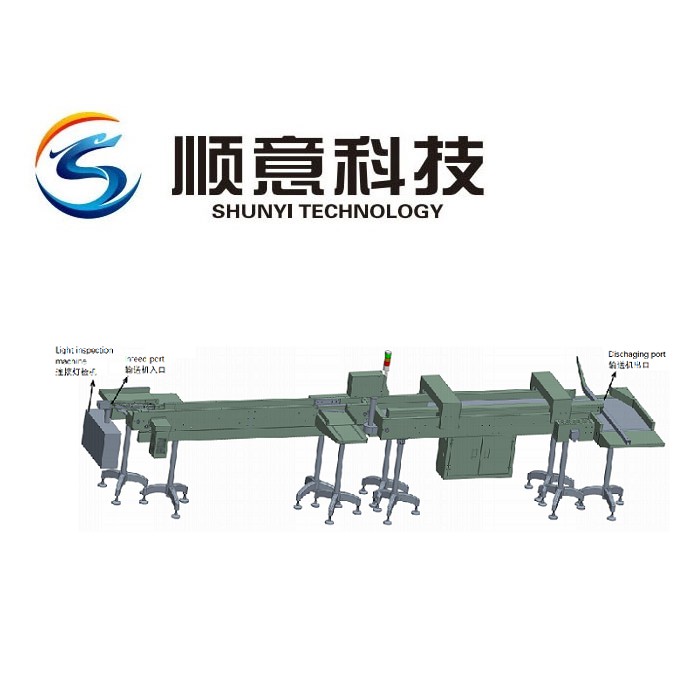

This adaptive speed feature is crucial in preventing jams because it allows the conveyor to respond to the dynamic nature of the production process. It ensures that the products are always moving at an appropriate speed for the current conditions.
3. Intelligent Sorting and Routing
In some production lines, products need to be sorted or routed to different destinations. Our intelligent conveyors are equipped with sorting mechanisms that can handle this task efficiently.
For example, there are diverters and pushers that can move products from one lane to another. These sorting devices are controlled by the conveyor's intelligent system, which uses data from the sensors to make decisions. If a particular product needs to be sent to a different packaging station, the system will calculate the best time and position to activate the sorting mechanism.
This intelligent sorting helps prevent jams by ensuring that products are evenly distributed across the conveyor. Instead of all the products trying to go through the same path and causing a bottleneck, they are smoothly directed to their respective destinations. In a Pharmaceutical Ampoule Conveyor, different types of ampoules can be sorted based on their size, dosage, or other criteria, reducing the chances of jams.
4. Self - Diagnostics and Predictive Maintenance
Our intelligent conveyors are not just good at preventing jams in the moment; they can also predict potential issues before they happen. The conveyor's control system has self - diagnostic capabilities that continuously monitor the health of the conveyor.
It can check the condition of the motors, belts, and other components. If it detects any signs of wear and tear, such as abnormal vibrations or changes in motor current, it will alert the maintenance team. This allows for proactive maintenance, where parts can be replaced before they fail and cause a jam.
For example, if the system notices that the belt tension is starting to change, it can schedule a maintenance check to adjust the tension. This predictive maintenance approach ensures that the conveyor is always in optimal condition, reducing the risk of jams due to mechanical failures.
5. User - Friendly Interface and Customization
We understand that every production line is different, and our customers may have specific requirements. That's why our intelligent conveyors come with a user - friendly interface that allows operators to customize the conveyor's settings.
Operators can set parameters such as the minimum and maximum speed, the distance between products, and the sorting rules. They can also monitor the conveyor's performance in real - time through the interface. If they see that a particular area of the conveyor is having issues, they can make manual adjustments if needed.
This customization feature is great because it gives our customers more control over their production process. They can fine - tune the conveyor to suit their specific products and production volume, further reducing the likelihood of jams.
6. Compatibility with Existing Systems
Our intelligent conveyors are designed to be compatible with existing production systems. Whether you have a small - scale operation or a large - scale factory, our conveyors can integrate seamlessly with your current equipment.
They can communicate with other machines in the production line, such as filling machines, labeling machines, and packaging machines. This communication ensures that the entire production process is synchronized. For example, the conveyor can adjust its speed based on the output of the Ampoule Bottle Conveyor to prevent jams at the transfer points between different machines.
Conclusion
So, there you have it! Our intelligent conveyors use a combination of smart sensors, adaptive speed control, intelligent sorting, self - diagnostics, user - friendly interfaces, and compatibility with existing systems to prevent product jams. They are a reliable solution for any production line that wants to improve efficiency, reduce downtime, and protect their products.
If you're looking for a way to optimize your production process and say goodbye to those frustrating product jams, we'd love to talk to you. Contact us for more information and let's start a discussion about how our intelligent conveyors can meet your specific needs.
References
- "Conveyor Belt Technology Handbook"
- "Automation in Manufacturing: Principles and Applications"
- Industry reports on pharmaceutical conveyor systems