

As a leading supplier of intelligent conveyors, I've witnessed firsthand the transformative impact these systems have on modern manufacturing and distribution processes. One of the most critical challenges in these operations is product stacking, which requires precision, efficiency, and adaptability. In this blog, I'll delve into how our intelligent conveyors handle product stacking, exploring the technology, benefits, and real - world applications.
Understanding the Challenge of Product Stacking
Product stacking is a complex task that involves arranging products in an organized manner, whether it's for storage, transportation, or further processing. In a manufacturing or distribution environment, products come in various shapes, sizes, and weights. For instance, in the pharmaceutical industry, ampoules, vials, and bottles need to be stacked carefully to prevent breakage. In the food industry, packages of different dimensions must be stacked efficiently to maximize space utilization.
Traditional conveyor systems often struggle with product stacking. They lack the flexibility to handle a wide range of products and may not be able to adjust to changing production requirements. This can lead to inefficiencies, such as product damage, uneven stacking, and wasted space.
How Intelligent Conveyors Address Product Stacking
Advanced Sensors and Vision Systems
Our intelligent conveyors are equipped with state - of the - art sensors and vision systems. These sensors can detect the size, shape, and position of each product as it moves along the conveyor. For example, laser sensors can measure the height and width of a product, while cameras can identify its orientation. This real - time data is then used to make precise decisions about how to stack the products.
The vision systems can also perform quality control checks during the stacking process. They can detect any defects or irregularities in the products, such as cracked ampoules or misaligned packages. If a defective product is detected, the conveyor can divert it from the stacking area, ensuring that only high - quality products are stacked.
Programmable Logic Controllers (PLCs)
PLCs are the brains of our intelligent conveyors. They receive data from the sensors and vision systems and use pre - programmed algorithms to control the stacking process. These algorithms can be customized based on the specific requirements of each application.
For example, if you need to stack products in a particular pattern, such as a pyramid or a grid, the PLC can adjust the speed and movement of the conveyor to achieve the desired result. It can also optimize the stacking process to minimize the use of space and maximize the stability of the stack.
Adaptive Conveyor Design
Our intelligent conveyors are designed to be highly adaptable. They can handle products of different sizes and weights without the need for extensive reconfiguration. For example, the conveyor belts can be adjusted to accommodate products of varying widths, and the height of the conveyor can be raised or lowered to match the stacking requirements.
In addition, our conveyors can be integrated with other equipment, such as robotic arms or palletizers. This allows for seamless automation of the stacking process, increasing efficiency and reducing the risk of human error.
Benefits of Using Our Intelligent Conveyors for Product Stacking
Improved Efficiency
By automating the product stacking process, our intelligent conveyors can significantly increase the speed and efficiency of your operations. They can stack products at a much faster rate than manual labor, reducing the time it takes to complete a production run.
In addition, the precise control provided by the sensors and PLCs ensures that products are stacked in the most efficient way possible. This can lead to a reduction in wasted space, allowing you to store more products in the same area.
Enhanced Product Quality
The advanced sensors and vision systems on our conveyors help to ensure that only high - quality products are stacked. By detecting and removing defective products before they are stacked, you can reduce the risk of product damage during storage and transportation.
This also improves customer satisfaction, as your customers will receive products that meet the highest quality standards.
Flexibility and Scalability
Our intelligent conveyors are designed to be flexible and scalable. They can be easily reconfigured to handle different products and production requirements. Whether you are expanding your business or introducing new products, our conveyors can adapt to your changing needs.
Cost Savings
While the initial investment in an intelligent conveyor system may be higher than that of a traditional conveyor, the long - term cost savings are significant. By increasing efficiency, reducing product damage, and improving quality, you can lower your operating costs and increase your profitability.
Real - World Applications
Pharmaceutical Industry
In the pharmaceutical industry, our intelligent conveyors are used to stack ampoules, vials, and bottles. The Pharmaceutical Ampoule Conveyor is specifically designed to handle the delicate nature of pharmaceutical products. It uses gentle handling techniques to prevent breakage and contamination.
The conveyor's sensors can detect the presence of each ampoule and ensure that they are stacked in a precise pattern. This is crucial for maintaining the integrity of the products and complying with strict regulatory requirements.
Food and Beverage Industry
In the food and beverage industry, our intelligent conveyors are used to stack packages of various sizes and shapes. The Ampoule Bottle Conveyor can be adapted to handle different types of packaging, such as cans, bottles, and cartons.
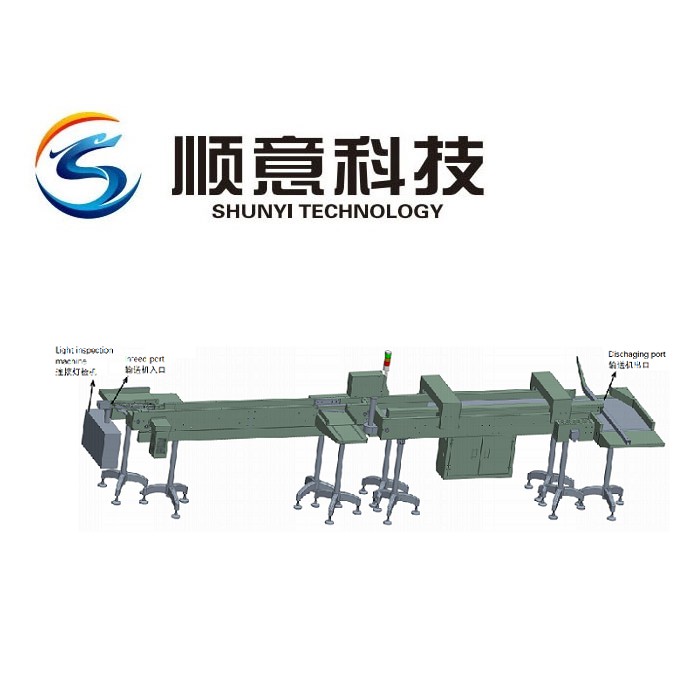

The conveyor's vision systems can check the labels and seals of the packages to ensure that they are correct and intact. This helps to prevent product recalls and maintain the quality of the food and beverage products.
Logistics and Distribution
In the logistics and distribution industry, our intelligent conveyors are used to stack pallets and containers. The Buffer Conveyor can store products temporarily and release them at the right time for further processing or shipping.
The conveyor's PLCs can optimize the stacking process to ensure that the pallets are stable and easy to handle. This improves the efficiency of the warehouse operations and reduces the risk of accidents.
Contact Us for Your Product Stacking Needs
If you're looking for a reliable solution to your product stacking challenges, our intelligent conveyors are the answer. We have a team of experts who can work with you to understand your specific requirements and design a customized conveyor system for your business.
Whether you're in the pharmaceutical, food and beverage, or logistics industry, our intelligent conveyors can help you improve efficiency, enhance product quality, and save costs. Contact us today to start a conversation about how we can meet your product stacking needs and take your operations to the next level.
References
- "Automated Conveyor Systems in Manufacturing: A Review", Journal of Manufacturing Technology, 2020
- "Advanced Sensors for Conveyor Belt Monitoring", Sensors and Actuators Journal, 2019
- "Programmable Logic Controllers in Industrial Automation", Industrial Automation Magazine, 2018