

Hey there! As a supplier of intelligent conveyors, I'm super excited to dig into how these nifty machines handle product labeling. It's a topic that's not only fascinating but also crucial for businesses looking to streamline their operations and boost efficiency.
First off, let's talk about what an intelligent conveyor is. It's not your average run - of - the - mill conveyor belt. These conveyors are equipped with advanced sensors, smart control systems, and often some form of automation. They can adapt to different product sizes, shapes, and weights, and they're designed to work in harmony with other parts of the production line, like labeling machines.
One of the key features of an intelligent conveyor when it comes to product labeling is its ability to precisely position products. You see, for a label to be applied correctly, the product needs to be in the right place at the right time. Our intelligent conveyors use sensors to detect the position and orientation of each product as it moves along the belt. These sensors can be optical, laser - based, or even ultrasonic, depending on the specific requirements of the application.
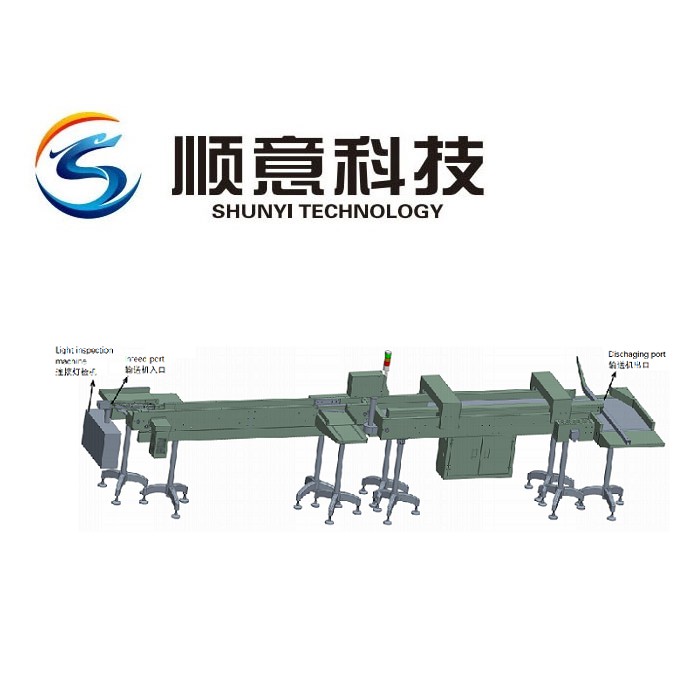
For example, if you're labeling small, delicate items like ampoules, the conveyor needs to be extremely accurate. That's where our Ampoule Bottle Conveyor comes in. It can gently transport ampoules and ensure they're perfectly aligned for labeling. The sensors on this conveyor can detect the slightest misalignment and make real - time adjustments to the speed and position of the belt.
Once the product is in the correct position, the conveyor works in tandem with the labeling machine. The intelligent conveyor can slow down or stop the product for a split second to allow the labeling machine to apply the label smoothly. This synchronization is crucial for high - quality labeling. Our conveyors are programmed to communicate with a wide range of labeling machines, whether they're pressure - sensitive label applicators, hot - stamp labelers, or wrap - around labelers.
Another important aspect is the speed control of the conveyor. In a production environment, you want to label as many products as possible in the shortest amount of time, but not at the expense of quality. Our intelligent conveyors can adjust their speed based on the type of label being applied and the complexity of the labeling process. For instance, if you're applying a large, multi - panel label, the conveyor might slow down to give the labeling machine more time to apply the label accurately.
Now, let's talk about handling different product shapes and sizes. Our intelligent conveyors are designed to be flexible. They can handle everything from round bottles to square boxes. The conveyor can adjust its width and the height of the side guides to accommodate different product dimensions. This is especially useful in industries like pharmaceuticals, where you might have a variety of product sizes and shapes. Our Pharmaceutical Ampoule Conveyor is a great example of this flexibility. It can handle different sizes of ampoules with ease, ensuring that each one gets labeled correctly.
In addition to positioning and speed control, our intelligent conveyors also offer quality control features. They can detect if a label is applied incorrectly or if there's a problem with the label itself. For example, if a label is wrinkled or has a tear, the conveyor can reject the product and divert it to a separate area for further inspection. This helps to maintain a high level of product quality and reduces waste.
We also have a Buffer Conveyor in our lineup. This conveyor is really handy when it comes to product labeling. It can store products temporarily, allowing the labeling machine to catch up if there's a backlog. This ensures a continuous flow of labeled products and prevents bottlenecks in the production line.
The software that runs our intelligent conveyors is another game - changer. It allows for easy programming and customization. You can set up different labeling programs for different products, and the conveyor will automatically adjust its settings based on the product being processed. This means that you can switch between different products quickly and easily, without having to make a lot of manual adjustments.
When it comes to maintenance, our intelligent conveyors are designed to be user - friendly. They have self - diagnostic features that can detect any potential problems early on. This helps to minimize downtime and keep your production line running smoothly. The sensors and control systems are also modular, which means that if something does go wrong, it can be easily replaced.
So, if you're in the market for an intelligent conveyor that can handle product labeling like a pro, you've come to the right place. Our conveyors are reliable, efficient, and flexible, and they can be customized to meet the specific needs of your business. Whether you're in the pharmaceutical, food and beverage, or consumer goods industry, we have a solution for you.

If you're interested in learning more about how our intelligent conveyors can benefit your product labeling process, don't hesitate to reach out. We'd love to have a chat with you and see how we can help you take your production line to the next level.
References
- Industry standards and best practices for conveyor systems in product labeling applications.
- Internal research and development reports on the performance of our intelligent conveyors.