

In the fast - paced world of modern industry, the ability to handle different types of products efficiently is a crucial factor for success. As a supplier of intelligent conveyors, I often encounter the question: Can an intelligent conveyor handle different types of products? The answer is a resounding yes, and in this blog, I will explore the various aspects that enable intelligent conveyors to manage diverse product types effectively.
Technological Features Enabling Product Diversity
One of the key technological features of intelligent conveyors is their adjustable speed and movement. Different products may require different transportation speeds. For example, fragile items such as glass ampoules need a slower and more stable movement to prevent breakage. Our intelligent conveyors can be programmed to adjust the speed according to the product's characteristics. The advanced control system allows for precise speed regulation, ensuring that each product is transported safely and efficiently.
Another important aspect is the customizable conveyor belt. Our intelligent conveyors come with a variety of belt options. For products with irregular shapes, we can provide belts with special surface textures or attachments. For instance, a belt with cleats can be used to prevent small or round products from rolling off during transportation. Moreover, the width and length of the conveyor belt can be customized to accommodate different product sizes. Whether it's a tiny electronic component or a large industrial part, our intelligent conveyors can be tailored to fit the specific requirements.
Handling Different Industries and Product Types
Pharmaceutical Industry
In the pharmaceutical industry, there is a wide range of product types, from small tablets to large vials. Our [Ampoule Bottle Conveyor](/pharmaceutical - conveyor/intelligent - conveyor/ampoule - bottle - conveyor.html) is specifically designed to handle ampoule bottles with high precision. These conveyors are made of materials that meet strict pharmaceutical hygiene standards. They are equipped with sensors to detect any misaligned or damaged ampoules, ensuring that only high - quality products move forward in the production line.
The [Pharmaceutical Ampoule Conveyor](/pharmaceutical - conveyor/intelligent - conveyor/pharmaceutical - ampoule - conveyor.html) also plays a vital role in the pharmaceutical manufacturing process. It can handle different sizes of ampoules, from 1ml to 10ml, with ease. The intelligent control system ensures that the ampoules are transported at a consistent speed, which is essential for filling, sealing, and labeling operations.
Food Industry
The food industry has its own unique requirements for product handling. Products can range from delicate pastries to heavy bags of flour. Our intelligent conveyors are designed to meet these diverse needs. For food products, the conveyor belts are made of food - grade materials that are easy to clean and sanitize. This helps to prevent cross - contamination between different products.
In the case of small, irregularly shaped snacks, the conveyor can be equipped with a gentle handling mechanism. It uses soft belts and slow - moving sections to ensure that the snacks are not crushed or damaged. For larger food items, such as boxes of cereal, the conveyor can handle high - volume transportation with high efficiency.
Electronics Industry
Electronics products are often small, lightweight, and sensitive to static electricity. Our intelligent conveyors are designed to address these challenges. They are equipped with anti - static materials to prevent damage to electronic components. The conveyor can also be configured with precision positioning systems, which are crucial for processes such as pick - and - place operations in electronics assembly.

Buffer and Storage Capabilities
In addition to transporting different products, intelligent conveyors also offer buffer and storage capabilities. Our [Buffer Conveyor](/pharmaceutical - conveyor/intelligent - conveyor/buffer - conveyor.html) can store products temporarily when there is a bottleneck in the production line. This is particularly useful in industries where production processes are not always synchronized. For example, if a packaging machine breaks down, the buffer conveyor can hold the products upstream, preventing a complete shutdown of the production line.
The buffer conveyor can be programmed to release products at a controlled rate once the downstream process is ready. This helps to maintain a continuous and efficient production flow, even when dealing with different product types.
Integration with Other Systems
Intelligent conveyors are not standalone devices. They can be easily integrated with other systems in the production line, such as robotic arms, sensors, and quality control devices. This integration allows for seamless handling of different products. For example, a robotic arm can pick up products from the conveyor based on specific criteria, such as size or weight. Sensors can detect product defects and divert faulty products to a separate area for further inspection.
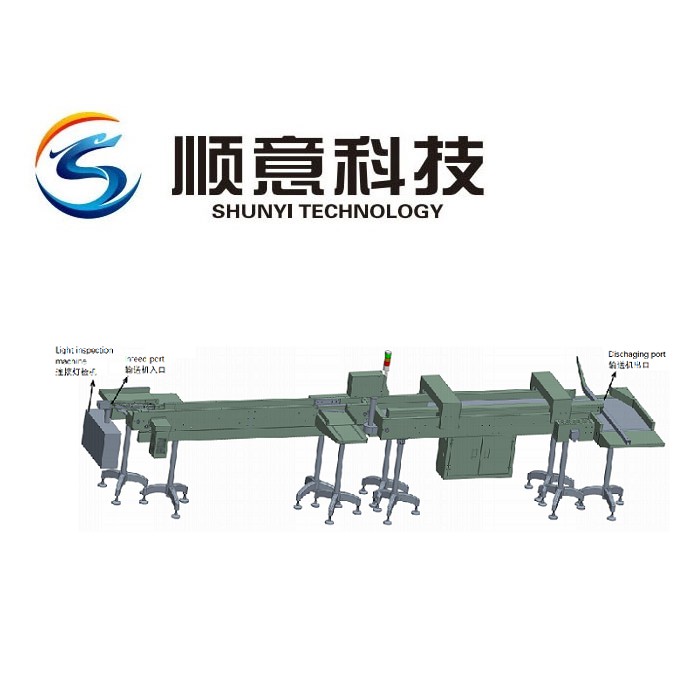
The ability to integrate with other systems also enhances the overall flexibility of the production line. As new product types are introduced, the conveyor system can be quickly reconfigured to work in harmony with other equipment, ensuring that the production process remains efficient and cost - effective.

Cost - effectiveness and Return on Investment
Investing in an intelligent conveyor system may seem like a significant upfront cost. However, in the long run, it offers substantial cost - savings. By being able to handle different types of products, a single conveyor system can replace multiple specialized conveyors. This reduces the need for additional equipment and maintenance costs.
Moreover, the increased efficiency and productivity of the production line lead to a higher return on investment. The ability to handle diverse products quickly and accurately means that more products can be produced in less time, resulting in increased revenue for the business.
Conclusion
In conclusion, intelligent conveyors are highly capable of handling different types of products. Their adjustable speed, customizable belts, and advanced control systems make them suitable for a wide range of industries, including pharmaceuticals, food, and electronics. The buffer and storage capabilities, along with the integration with other systems, further enhance their versatility.

If you are looking for a reliable solution to handle different product types in your production line, our intelligent conveyors are the ideal choice. We are committed to providing high - quality, innovative conveyor systems that meet your specific needs. To learn more about our products and how they can benefit your business, please contact us for a procurement discussion.
References
- "Conveyor Systems Handbook" by John A. Reed
- "Automation in Industrial Manufacturing" by Peter J. Smith
- Industry reports on conveyor technology and its applications in different sectors.